IN Brief:
- EMD Electronics has opened a 38,000 sq ft semiconductor materials R&D facility at Sheboygan Falls, Wisconsin.
- Eight laboratories cover discovery, development, qualification, analytical work, purification, packaging and hazard testing.
- The site combines synthesis, scale-up and technology transfer to move materials towards customer qualification and commercial production.
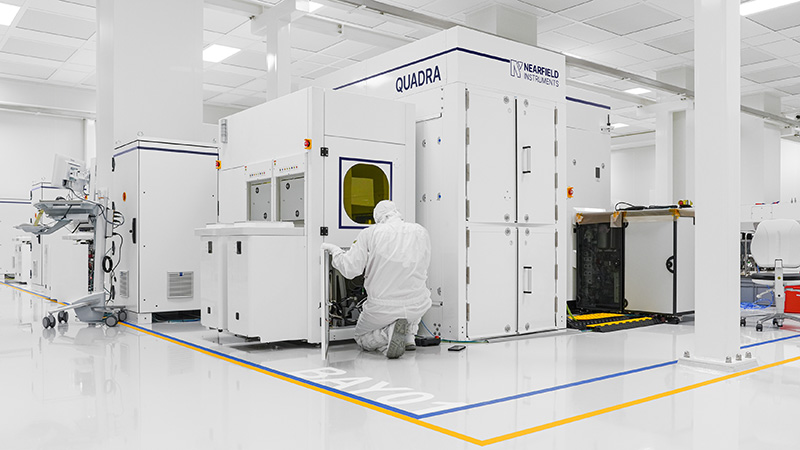
EMD Electronics has opened a 38,000 sq ft research and development facility in Sheboygan Falls, Wisconsin, combining semiconductor materials discovery with scale-up, qualification and technology transfer needed to move new chemistries towards production.
The facility contains eight dedicated laboratories covering discovery, development, qualification, analytical development, purification, packaging and hazard testing. Placing those activities at one site reduces the number of physical and organisational transfers between synthesising a candidate material and establishing whether it can be manufactured, handled and qualified consistently enough for semiconductor production.
A chemistry that performs well on a small experimental sample still has to remain stable as batch size increases, meet increasingly demanding purity requirements and behave predictably inside production equipment. New device structures add further interfaces and processing steps, making material consistency more difficult to separate from the electrical performance of the resulting semiconductor.
Scale-up therefore creates a different engineering problem from discovery. Larger reaction volumes can change mixing, heat transfer and impurity behaviour, while production equipment may expose the chemistry to surfaces and operating conditions that were absent from the original laboratory experiment.
The Wisconsin facility brings those development stages closer together so that such limitations can be identified before a material enters customer qualification. Synthesis, purification and analytical work can be adjusted alongside scale-up rather than passing the chemistry between separate locations after each iteration.
Technology transfer then converts a successful laboratory process into manufacturing instructions capable of producing the same material repeatedly. Raw material specifications, reaction conditions, purification steps, analytical tests and packaging requirements all have to remain within defined limits if a semiconductor fab is to receive consistent material from one delivery to the next.
EMD Electronics supplies materials including specialty gases, deposition products and chemistries used in planarisation and patterning. Although they enter fabrication at different stages, each category requires tight contamination control because trace metals, particles or unwanted chemical species can alter film properties, create defects or reduce yield.
Analytical development consequently sits alongside synthesis rather than acting only as a final quality check. A new material needs measurement methods capable of detecting the impurities, composition changes and physical characteristics that determine whether one experimental batch is genuinely equivalent to another.
Customer qualification extends the same work into the fab process. A manufacturer cannot normally substitute a critical material solely because it performs well in the supplier’s laboratory; the change has to be evaluated against deposition, patterning, cleaning, electrical performance and yield within the customer’s own integration flow.
Locating synthesis and scale-up within the same R&D operation can shorten the response when qualification exposes a compositional or processing issue. Engineers can modify the material and produce another controlled batch without transferring the problem back through a separate development and manufacturing chain.
The Wisconsin expansion forms part of a $200 million multi year investment across EMD Electronics’ US operations. Further work at Sheboygan Falls is scheduled for completion in 2027, alongside projects already completed at Carlsbad, California, and Catoosa, Oklahoma. The programme sits within a broader $1 billion US investment announced by the company in 2021.
EMD has also incorporated environmental controls into the laboratory design and says the operation uses renewable electricity while targeting LEED Gold certification. Laboratory energy demand can be substantial because ventilation, fume handling, purification and controlled processing operate continuously around experimental and pilot equipment.
The technical performance of the facility will ultimately be measured by how reliably promising materials can move from experimental synthesis into repeatable customer qualification. Semiconductor process materials disappear from view once they become part of a manufacturing recipe, but their purity and behaviour can determine whether a new transistor, interconnect or patterning process delivers acceptable yield.
EMD’s eight-laboratory model places discovery, analytical work, scale-up and qualification within one development environment. The facility is now operational, with the next stage of the Sheboygan Falls expansion scheduled to follow in 2027.